Cold-Rolled Coil Packing: Moisture Control Done Right
A correct wrapping recipe cannot fix a wet coil or rough handling. This guide links pre-pack dry condition, temporary storage rules, and post-pack discipline into one auditable cold-rolled packing process.
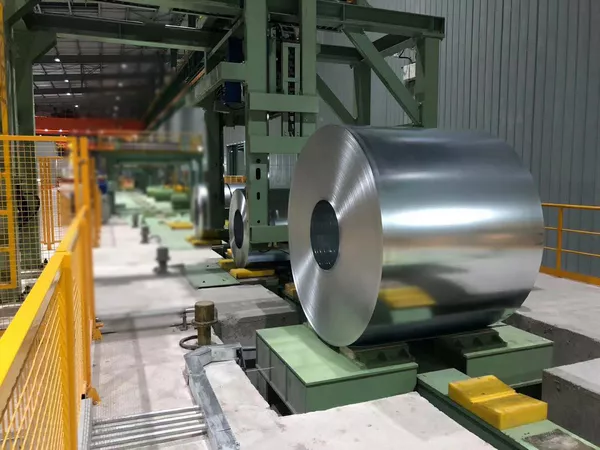
Cold-Rolled Steel Coil Packing: Moisture and Handling Control
Cold-Rolled Steel Coil Packing: Moisture and Handling Control
Cold-rolled coils often enter packaging with higher appearance expectations than hot-rolled products, but without the extra coating layer that can hide or absorb process mistakes. That means packaging quality depends heavily on two linked controls: the coil must enter packing in an acceptable dry condition, and the handling and temporary storage around the line must not reintroduce moisture or mechanical damage before release.
This article helps packaging, warehouse, and quality teams define cold-rolled coil packing on an automatic coil packing line as a controlled process rather than as a simple wrapping step.
Start with the Pre-Pack Condition
The package process should define what "ready for packing" means for a cold-rolled coil. That usually includes a confirmed identity, acceptable visible condition, and a dry state suitable for the approved packaging recipe. If the coil arrives wet, has visible condensation, or has been exposed to uncontrolled waiting conditions, the line should not treat it as a normal input.
This is where many packaging problems begin. Teams often discuss film, paper, or VCI while skipping the question of whether the coil was in the right condition before those materials were applied.
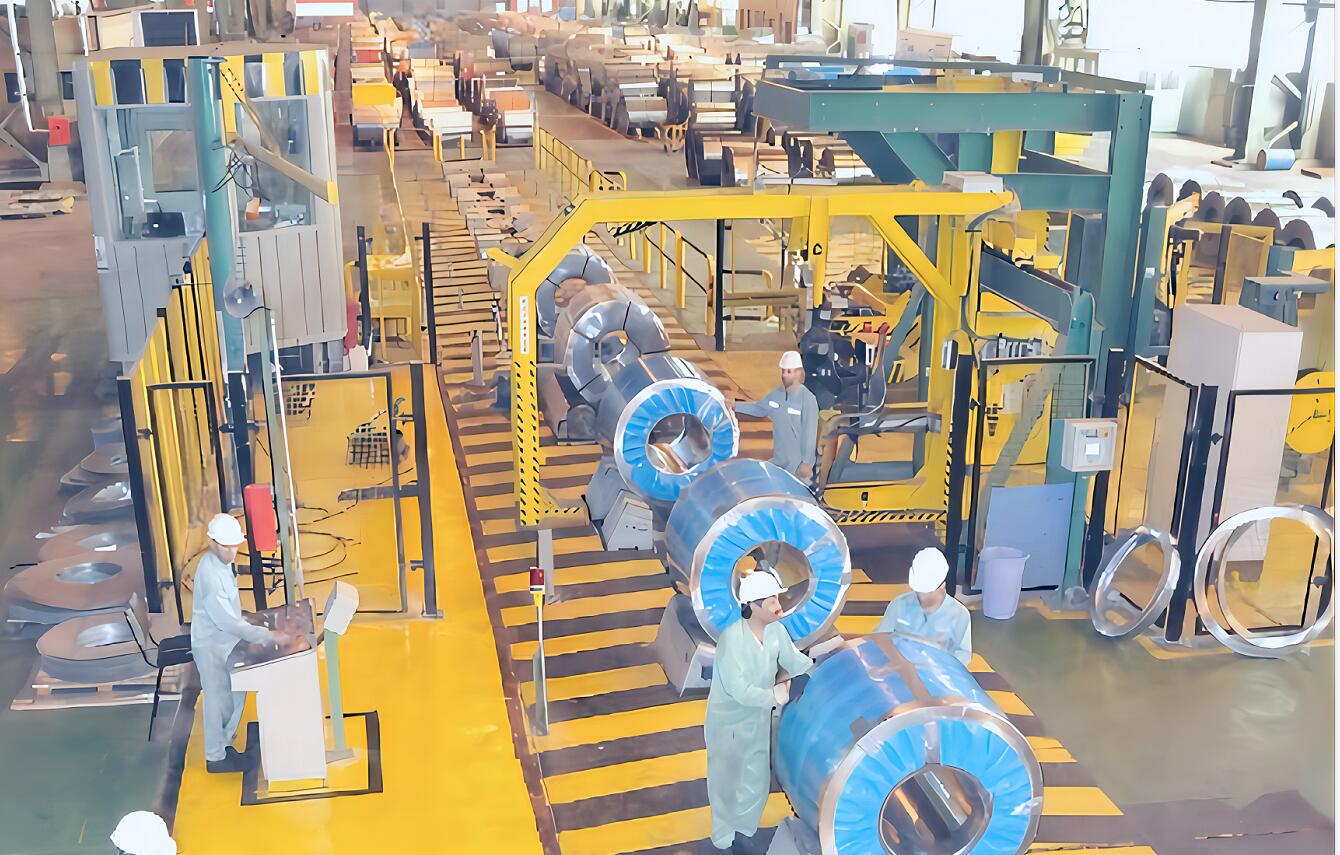
The image shows a cold-roll steel coil packing line. The process should begin with a confirmed dry condition and identity at the infeed, not assume the wrapper can correct a wet or doubtful coil.
Moisture Control Begins Before the Wrapper
Cold-rolled coils can be affected by condensation, uncontrolled dwell time, or movement between areas with different ambient conditions. A package process should define how the coil is staged before packing, who may release it into the line, and what happens if the coil does not meet the dry-condition rule.
Useful control points include:
- Where coils may wait before packing
- How long they may remain in an uncontrolled staging area if the site uses such a rule
- What visible or procedural check confirms acceptable pre-pack condition
- The abnormal route for a wet or doubtful coil
These controls are more important than any broad claim about moisture resistance.
Match the Package to Storage and Handling Reality
Cold-rolled products are often sensitive to both moisture-related risk and handling marks. The package should therefore be defined around the full route: packaging area, temporary storage, forklift or crane movement, warehouse dwell, and shipment preparation.
That route affects decisions about contact layers, outer wrap, edge protection, strapping arrangement, and release timing. A coil prepared for short internal transfer may not use the same recipe as one entering extended storage or export preparation.

The image shows a cold-rolled steel coil strapping machine. Strapping arrangement and contact layers should follow the full route, including temporary storage, lifting, warehouse dwell, and shipment preparation.
Temporary Storage Is Part of the Packaging Boundary
Many teams stop their process map at package completion. For cold-rolled material, temporary storage before dispatch can be just as important. If coils are staged in an unsuitable area, exposed to condensation risk, or handled repeatedly without controlled support, the final package result can degrade after the line has technically finished its job.
That is why a practical packaging rule should state where packaged coils may be staged, what support condition is required, and which events trigger reinspection before shipment.
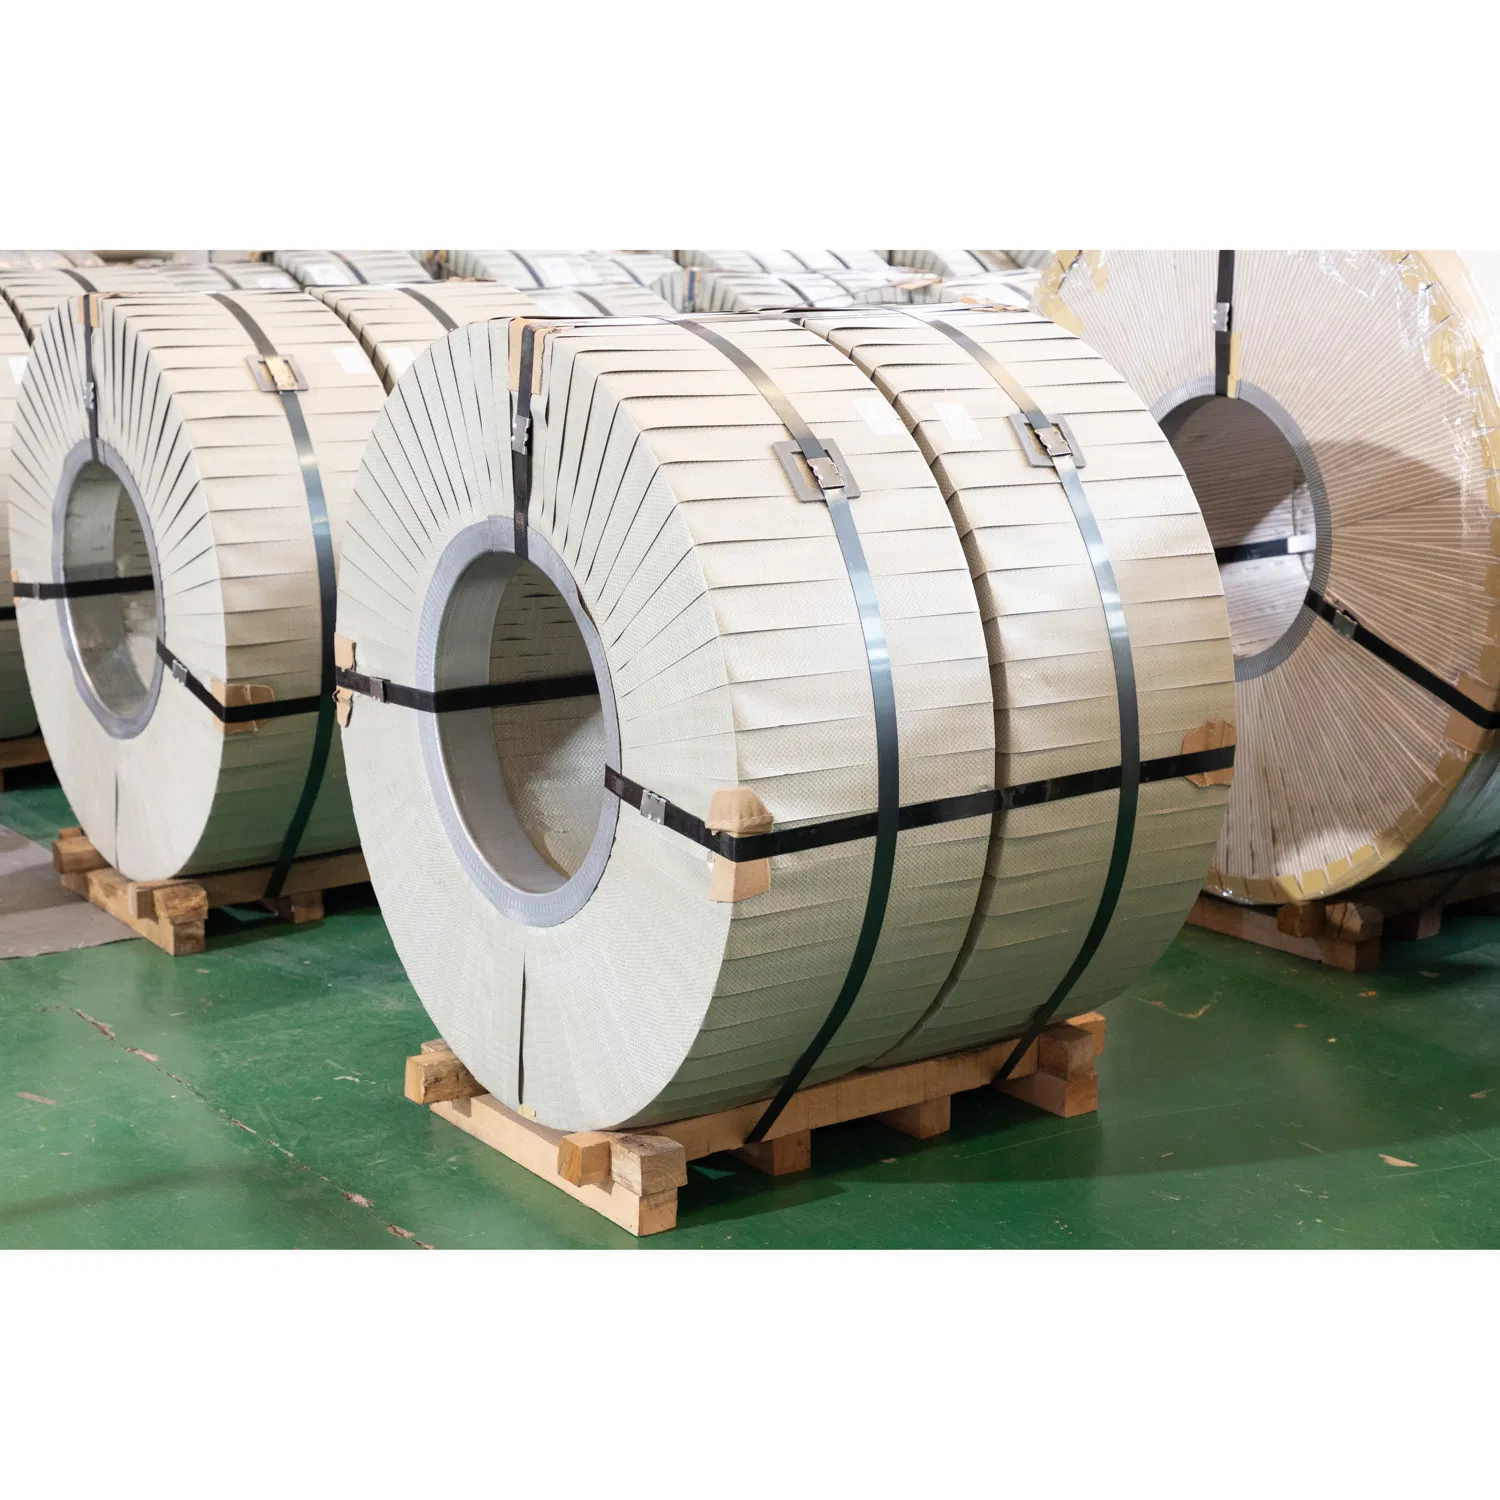
The image shows oriented standard export steel coil packing for silicon steel lamination. Temporary storage and dispatch preparation are part of the package boundary, because a finished package can degrade if staged under uncontrolled conditions.
Packaging-Area Discipline Supports Moisture Control
The packaging area itself should not be treated as a neutral background. If coils move from one ambient condition into another, if finished packages wait near open doors or uncontrolled transfer zones, or if identification and release are delayed, the moisture-control logic becomes weaker even when the wrapping recipe is correct.
For that reason, the process should define the handoff between incoming staging, packaging, and finished-goods staging clearly. The team should know where responsibility changes, what condition is checked at each handoff, and when a coil must be held instead of pushed forward just to keep the line moving.
Handling Control Matters as Much as Wrapping Control
Cold-rolled surfaces may be marked by unstable supports, slipping protectors, rough transfer, or repeated repositioning. A correct package recipe cannot compensate for poor movement discipline.
The process should define:
- Approved lifting or transfer method after packing
- Support and contact conditions during staging
- What to do when the package is disturbed or partially damaged
- Who decides whether repacking or reinspection is required
This keeps handling inside the packaging quality boundary instead of leaving it to informal practice.
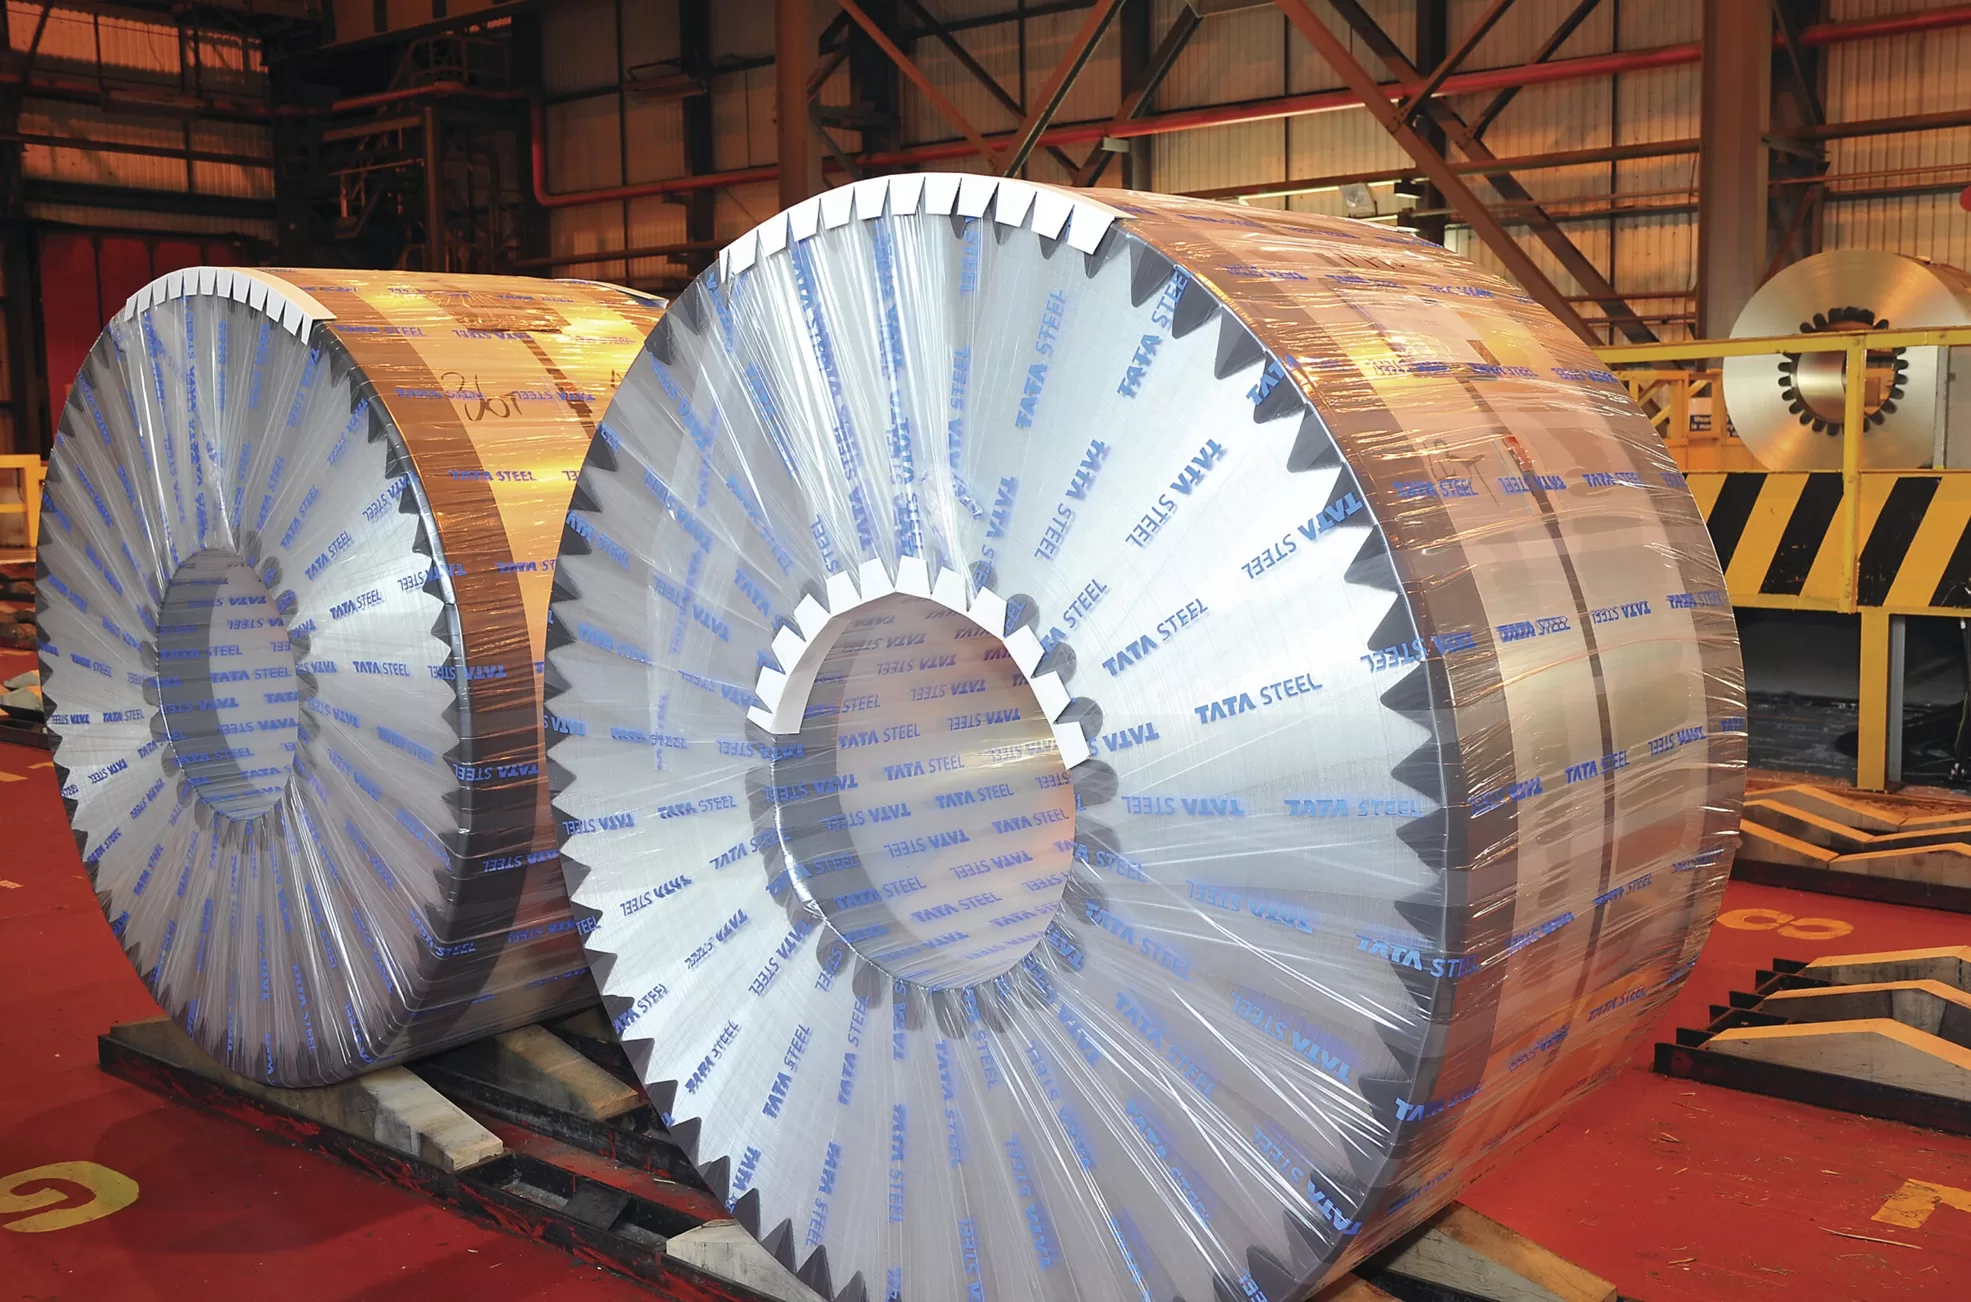
The image shows cold-roll coil packing with film wrapping. The correct recipe cannot compensate for poor movement discipline, so approved lifting, supports, and reinspection rules belong in the same process.
Watch a steel coil car for the cold roll packing line:

Release Should Be Conditional, Not Automatic
A finished cold-rolled package should not be released simply because the wrapping cycle ended. Release should depend on the verified package condition, label and traceability status, and the controlled post-pack route. If the intended storage area is not available or the package condition is doubtful, the coil should follow a defined hold route.
This is a process-control question, not only a quality question.
Acceptance Must Include Moisture and Post-Pack Flow
Acceptance for a cold-rolled package process should include more than a visual check at the wrapper. It should verify the handoff from pre-pack condition to post-pack route.
Useful evidence includes:
- Pre-pack dry-condition confirmation
- Correct recipe and contact materials
- Final package inspection
- Approved staging or dispatch route
- Reinspection rule after exceptional storage or handling
- Defined hold and release process
Those checks make the process auditable without overstating protection performance.
A Practical Next Step
Write a cold-rolled packaging rule that links three stages: dry-condition release into packing, controlled post-pack handling, and staging/dispatch release. Then test the rule with a real case that includes waiting time and warehouse movement on the automatic coil packing line, because that is where moisture and handling gaps usually appear.
Visual Details

Click to enlarge

Click to enlarge

Click to enlarge

Click to enlarge
Watch How It Works
Discover how our automated packaging solutions optimize your production line efficiency. This video demonstrates the seamless operation designed for maximum protection.
Trusted by Steel Mills & Industry Leaders
Global manufacturers rely on FHOPE heavy duty packaging equipment


Ready to optimize your packaging line?
Get a custom quote with ROI analysis. Our engineers respond within 24 hours.
- Free layout design
- Global installation support
- 2-year warranty included
Your information is secure and will never be shared.
Related Machines
Steel Coil Packaging line
View Details →
Vertical coil packaging line
View Details →
Hose Coil Packaging line
View Details →
Copper Coil Packaging line
View Details →
Wire Coil Packaging line
View Details →
Panel Packaging line
View Details →
Pipe Bagging Machine
View Details →
Aluminum profile packing line
View Details →
FHOPE Automatic pipe tube bundling&strapping line
View Details →
Automatic pipe tube bundling & strapping line
View Details →
Automatic steel tube strapping machine
View Details →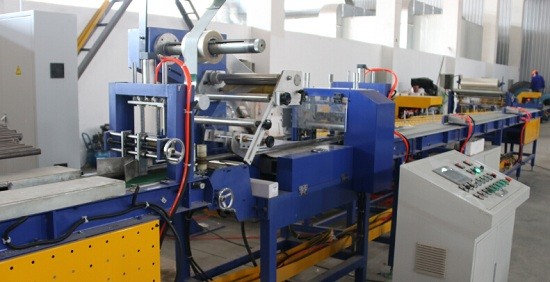
FHOPE Automatic steel tube packing machine
View Details →
Automatic plastic Pipe strapping packing line
View Details →
Automatic PPR/PVC Pipe bagging line
View Details →
Platsic pipe bag packing machine
View Details →
Tyre Packing Machine FPT-200
View Details →
Tyre Packing Machine FPT-300
View Details →
Tyre Packing Machine FPT-400
View Details →
Cable Coil Packing Machine-FPCA100
View Details →