Coil Stacking and Palletizing: What to Specify
A line can wrap a coil perfectly and still fail at the stacker. This specification guide covers stack rules, pallet interfaces, exceptions, data release, and FAT/SAT acceptance for the final load.
Automatic Coil Stacking and Palletizing: What to Specify
Automatic Coil Stacking and Palletizing: What to Specify
Stacking and palletizing are often added to a coil packing line after the wrapping scope is already discussed. That sequence creates avoidable problems. A line can wrap a coil correctly and still fail at the end of the process if the stack is unstable, the pallet interface is unclear, or the discharge area cannot absorb normal production.
This guide helps project, packaging, and logistics teams write a stacking and palletizing scope for an automatic coil packing line that can actually be reviewed and accepted.
Define the Final Unit Load First
Before discussing the stacker, define the final package that must leave the line. Ask:
- Is the output a single packed coil, a multi-coil stack, or a bundled palletized load?
- What is the maximum number of coils in one unit?
- What base, separator, or support material is required?
- How should labels remain visible after stacking?
- What handling method will be used after discharge?
The stacker should be designed around the final unit load, not the other way around.

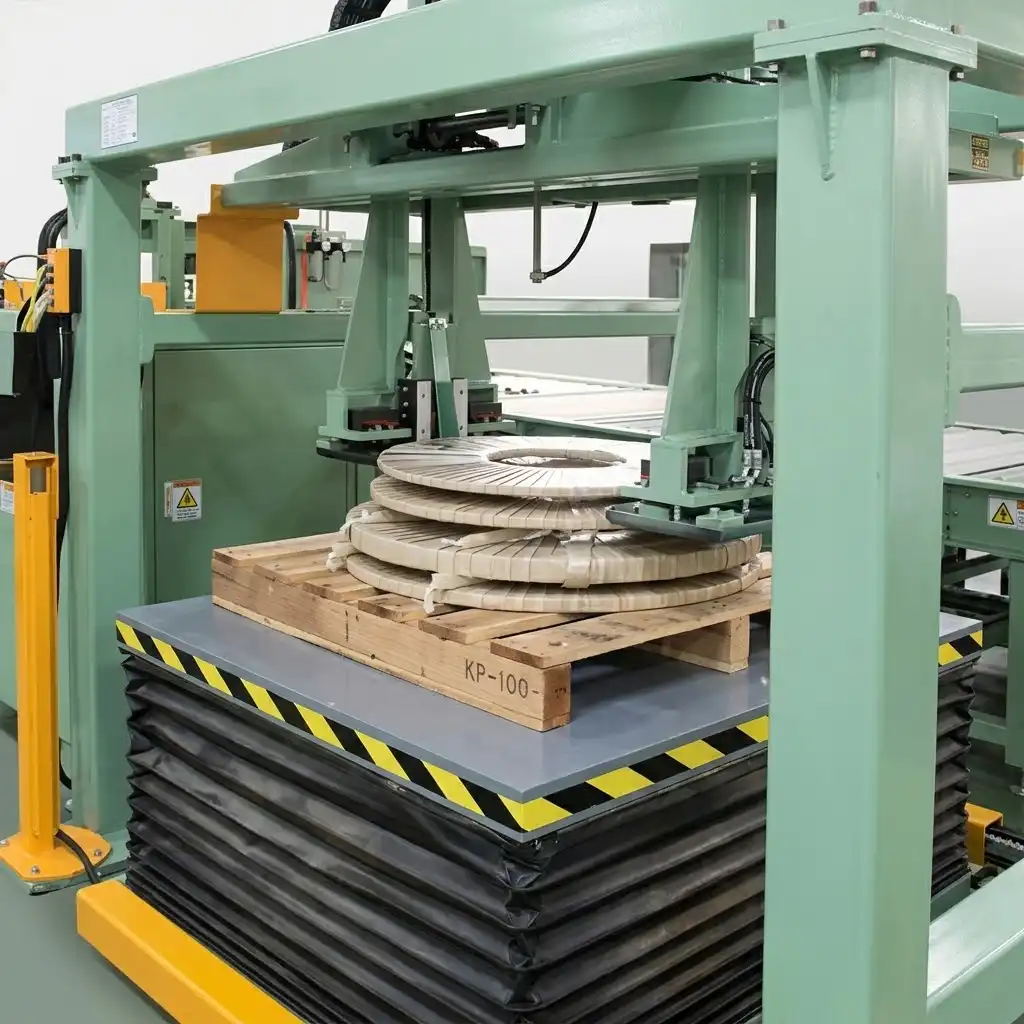
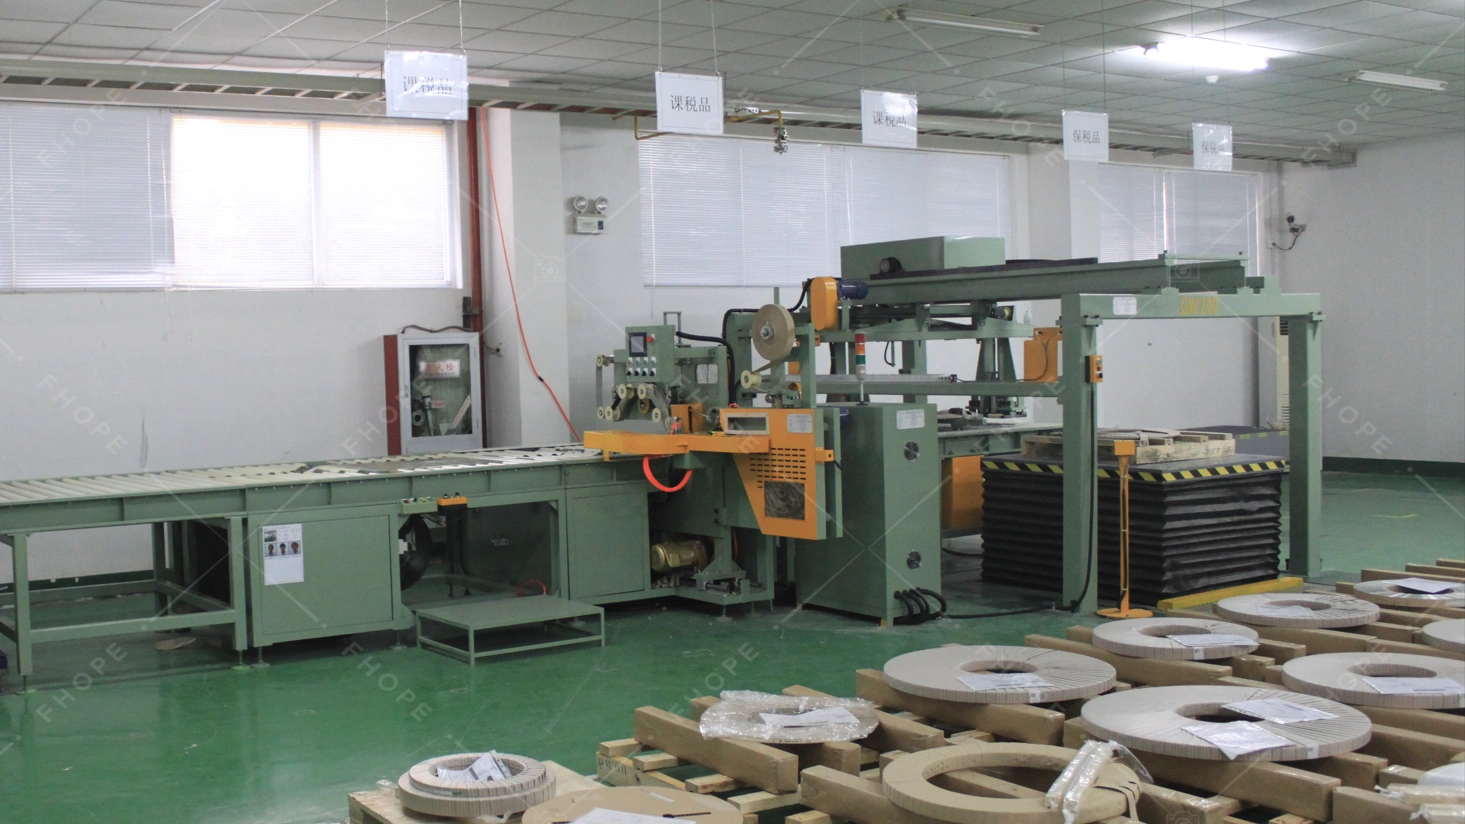
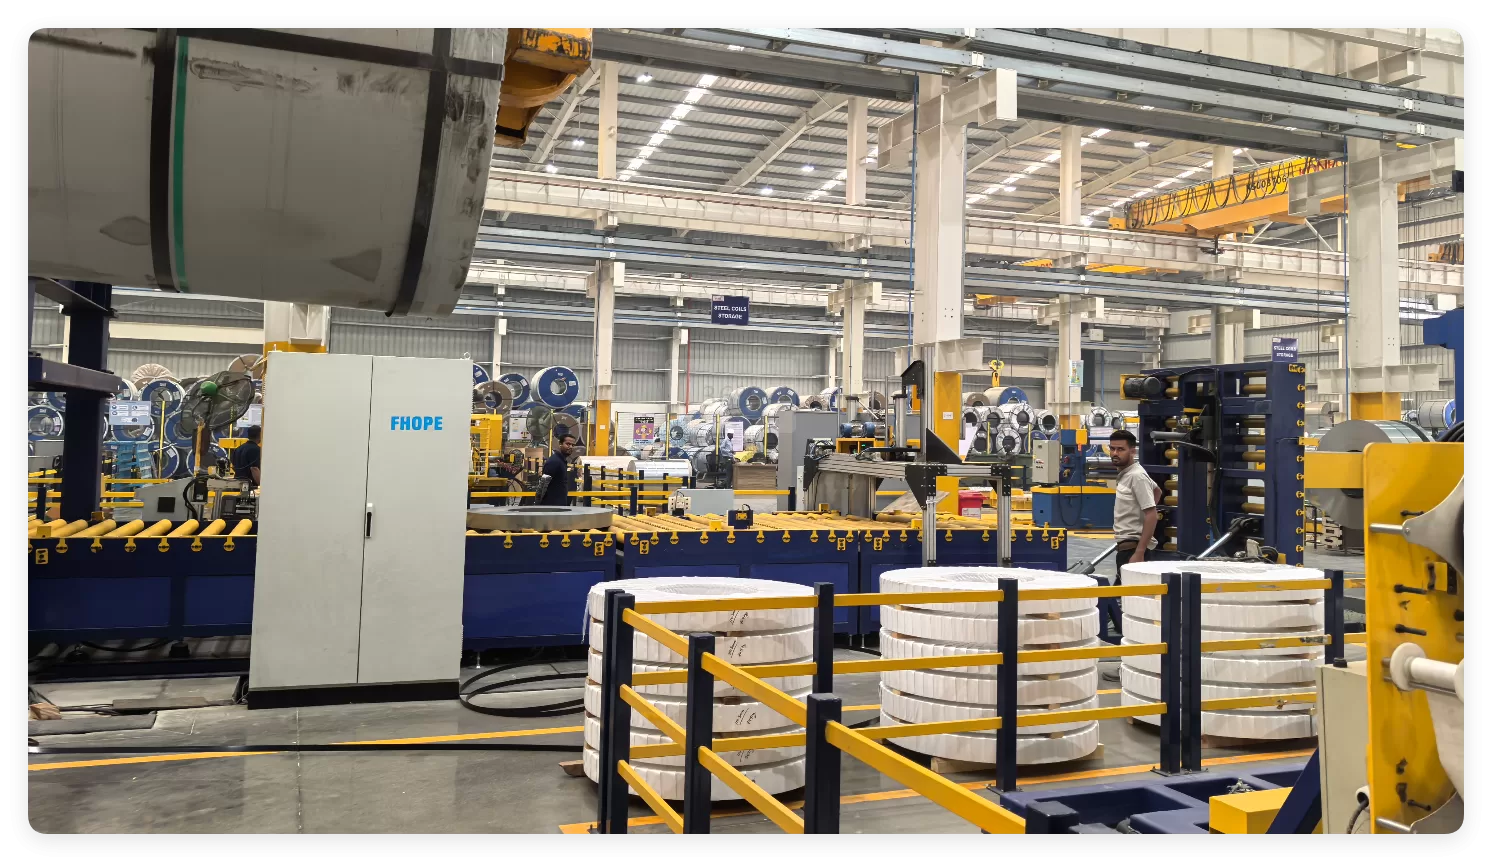
The image shows an automatic steel coil strapping and stacking conveyor line. The final unit load must be defined first so this line can be specified around the stack it has to produce.
Describe the Product Population That Enters the Stack
Stacking logic depends on the real coil mix. Width, outer diameter, weight, edge condition, surface sensitivity, and orientation all affect how coils may be combined. If the line processes multiple product families, the specification should state which ones may share a stack and which must remain separate.
Do not write only one maximum size. A good specification explains the combinations that actually occur.
State the Stack Rule Clearly
Many problems come from an unwritten stacking rule. The project document should say:
- How coils are grouped into one stack
- Whether stacking follows order, size, destination, or packaging recipe
- What the maximum stack height or count is for each family
- Which separators, pads, or base supports are required
- Which conditions force a manual or alternate route
If the line cannot determine those rules from the available order and product data, the automation scope is incomplete.
Define the Pallet or Base Interface
"Palletizing" may mean wood pallets, steel bases, skids, saddles, or custom supports. The line should specify what arrives at the station, how the base is positioned, who supplies it, how its identity is tracked if needed, and what happens when the correct base is missing.
Base loading and alignment are not minor details. A well-wrapped stack can still be rejected if it lands on the wrong support or in the wrong position.

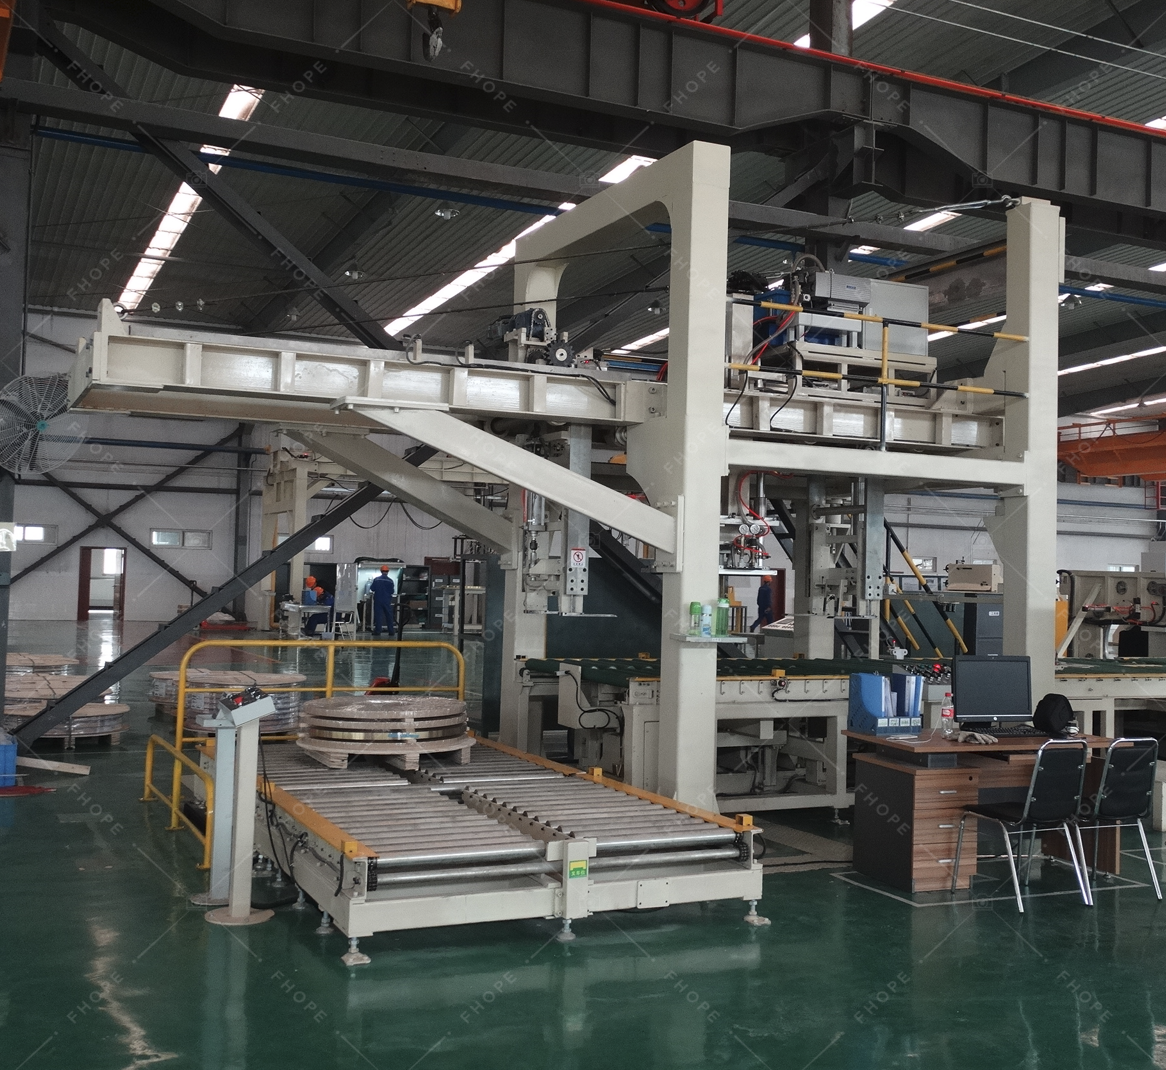
The image shows a steel coil pallet stacking line. The pallet or base interface, including who supplies it and how it is tracked, must be part of the same specification.
Protect the Stack During Transfer
The stack must survive more than the moment of placement. It has to remain stable during discharge, staging, forklift pickup, crane lifting where applicable, and storage. That means the stack design should define the contact points, center of support, separator behavior, and the way strapping or wrapping contributes to the final load.
Acceptance should be based on the finished unit load after handling, not only on the stacker's placement accuracy.
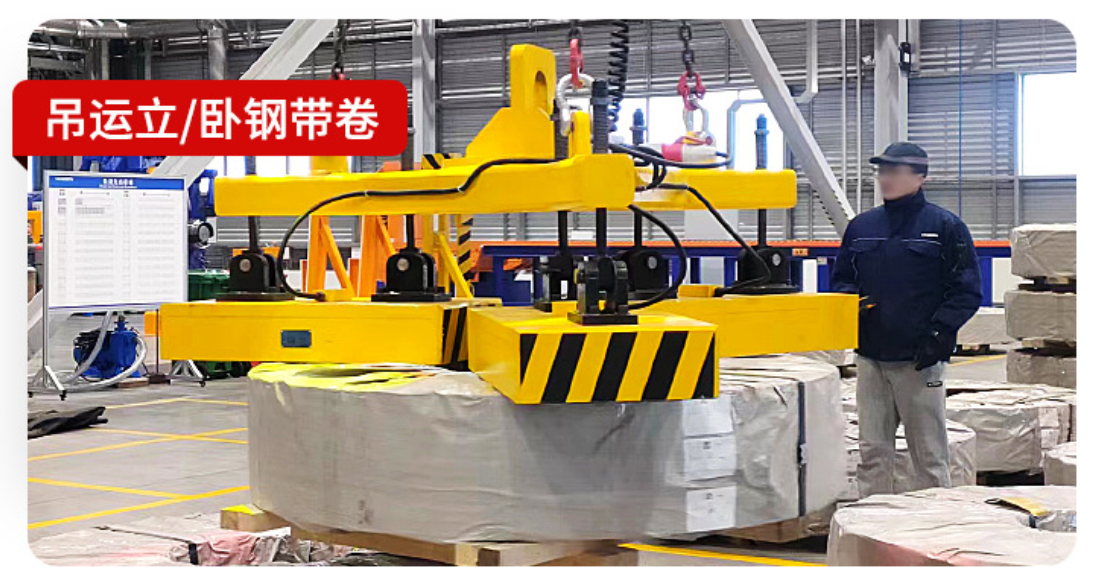
The image shows a coil magnet stacking machine with an operator nearby. The stack must survive the transfer method used here, so contact points, center of support, and release authority need to be defined before the machine starts.
Watch an automatic heavy-duty steel coil strapping and stretch wrapping line:

Include Exceptions and Mixed Conditions
What happens when one coil in the intended stack fails inspection, has a label mismatch, or requires a different route? What happens when the target pallet is unavailable? Those cases should be written into the scope before the logic is frozen.
Without an exception rule, the line will appear complete in a clean demo and become unstable in real production.
Connect Stacking to Data and Release
The stack output should keep the coil identity, quantity, package status, and shipping or storage destination aligned. The specification should identify the source of that data, when the stack is considered complete, and who may release it if one data field is missing or inconsistent.
This is especially important when the stack becomes the unit for weighing, labeling, warehousing, or shipment.
Define Who Owns the Last Decision
Automatic stacking does not remove responsibility for the final load. The project should identify who confirms the stack rule, who may override it, and who handles a mixed or blocked condition. In some plants that owner is operations; in others it is packaging or logistics. The point is not the department name. The point is that the release authority exists before the system goes live.
This also prevents a common startup problem where the machine completes the stack but no one is sure whether it may be moved.
Write Acceptance Around the Final Load
For FAT or SAT, test representative stack families and edge cases. Include:
- Minimum and maximum coil counts where applicable
- The most sensitive product surface
- The lightest and heaviest approved stack cases
- A missing base or wrong-base scenario
- An interrupted stack sequence and controlled recovery
The goal is to prove a stable, traceable final load, not only a functioning robot or stacker mechanism.
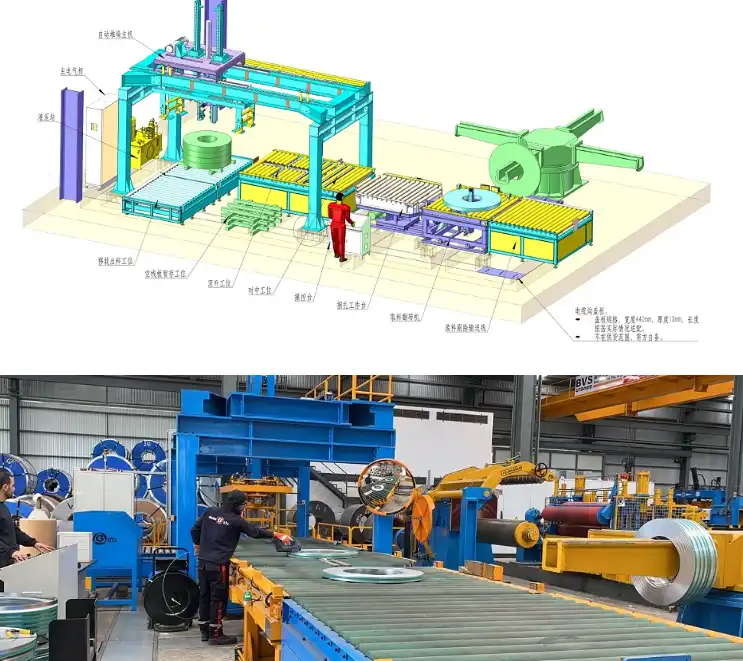
The image shows a slit coil handling and stacking line. Acceptance should be based on this final load after real handling, including the mixed conditions and interrupted sequences that occur in production.
Specification Page Skeleton
Keep one project page that records the decisions above in a form reviewers can check:
| Specification Field | What to Record |
|---|---|
| Final unit load | Single coil, stack, or palletized load |
| Grouping rule | Order, size, destination, or recipe |
| Base interface | Pallet, skid, saddle, supplier, and identity |
| Exception path | Failed coil, missing base, interrupted stack |
| Data and release | Identity, quantity, status, and release owner |
A Practical Next Step
Add a stacking specification page to the project file that defines the final unit load, grouping rules, base interface, exception routes, and acceptance evidence. Review it with packaging, logistics, and operations before the automatic coil packing line scope is finalized.
Visual Details

Click to enlarge
Click to enlarge
Click to enlarge
Click to enlarge
Watch How It Works
Discover how our automated packaging solutions optimize your production line efficiency. This video demonstrates the seamless operation designed for maximum protection.
Trusted by Steel Mills & Industry Leaders
Global manufacturers rely on FHOPE heavy duty packaging equipment


Ready to optimize your packaging line?
Get a custom quote with ROI analysis. Our engineers respond within 24 hours.
- Free layout design
- Global installation support
- 2-year warranty included
Your information is secure and will never be shared.
Related Machines
Steel Coil Packaging line
View Details →
Vertical coil packaging line
View Details →
Hose Coil Packaging line
View Details →
Copper Coil Packaging line
View Details →
Wire Coil Packaging line
View Details →
Panel Packaging line
View Details →
Pipe Bagging Machine
View Details →
Aluminum profile packing line
View Details →
FHOPE Automatic pipe tube bundling&strapping line
View Details →
Automatic pipe tube bundling & strapping line
View Details →
Automatic steel tube strapping machine
View Details →
FHOPE Automatic steel tube packing machine
View Details →
Automatic plastic Pipe strapping packing line
View Details →
Automatic PPR/PVC Pipe bagging line
View Details →
Platsic pipe bag packing machine
View Details →
Tyre Packing Machine FPT-200
View Details →
Tyre Packing Machine FPT-300
View Details →
Tyre Packing Machine FPT-400
View Details →
Cable Coil Packing Machine-FPCA100
View Details →